
Choosing Thermal Barrier Materials for Kilns: Temperature and Heat Loss




The best thermal barrier for a kiln is the lining system that keeps heat loss within an acceptable range while surviving the temperature, chemistry, mechanical loads and operating cycles at each layer. A material with a higher maximum temperature rating may be less effective as insulation, while a highly insulating product may fail if it is placed directly against an abrasive or chemically aggressive process.
For most evaluations, start by defining the hot-face duty and then work outward toward the shell. Compare complete lining arrangements at their expected temperatures, rather than selecting a material from a single conductivity figure. The preferred arrangement may combine a dense working lining with a lighter insulating layer, but that choice depends on available thickness, shell temperature limits and how the kiln is operated.
Start with the temperature each layer will experience
Kiln operating temperature is only the beginning of the specification. The hot face may experience local peaks above the temperature indicated by a process sensor, particularly near burners, flame impingement zones or other areas of uneven heat input. The evaluator needs a credible operating range for each zone, including normal conditions, expected excursions and the duration of those excursions.
Material temperature ratings must then be interpreted in the context of their test methods and intended use. A published maximum service temperature is not a guarantee that the product will retain acceptable strength, dimensions or insulating performance throughout a long campaign. Ask what happens near that limit: permanent shrinkage, loss of strength, reactions with adjacent materials and other changes can be more important than the headline rating.
Backing insulation does not see the full kiln temperature, but its hot-face temperature can still be too high. It depends on the conductivity and thickness of the working lining, the heat flow through the wall and the temperature at the outside surface. If the working lining becomes thinner through wear, the temperature at the insulation interface can rise. A design based only on the as-built thickness may therefore be inadequate later in the campaign.
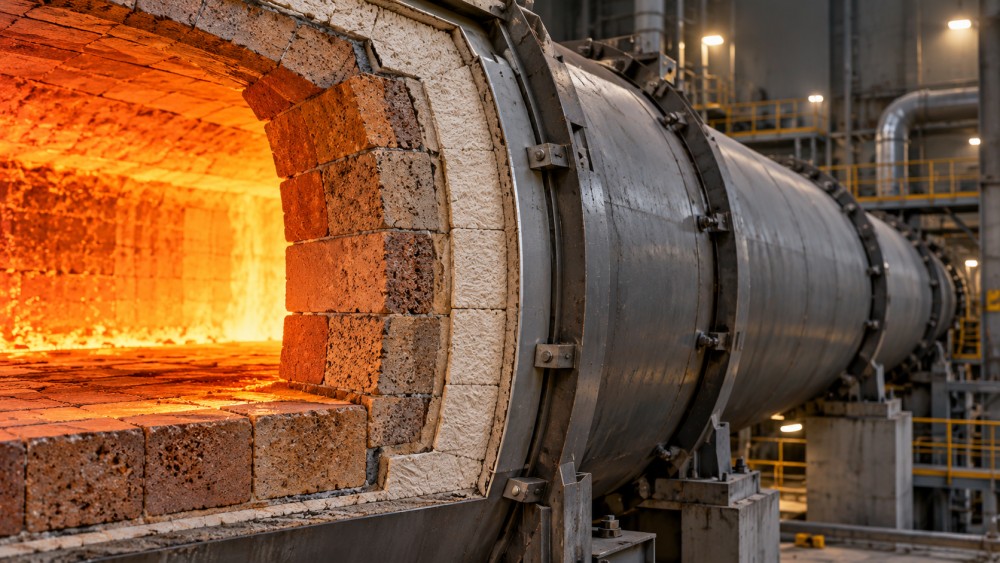
For a cylindrical kiln, temperature and heat flow should be assessed using the actual wall geometry and layer sequence. A flat-wall calculation can be useful for an initial comparison, but the final assessment should account for curvature where it materially affects the result. Rotary kilns also impose movement and mechanical loading that a static wall calculation cannot capture.
Compare heat loss across the whole lining
Thermal conductivity is central to the choice of thermal barrier materials for kilns, but a single value can be misleading. Conductivity changes with temperature, and each layer operates across a temperature range. Compare products using conductivity data relevant to those temperatures and, where available, to the installed density and expected condition of the material.
For an initial comparison, a thicker layer of lower-conductivity material generally offers greater resistance to heat flow. In a multilayer lining, however, changing one layer also changes interface temperatures. Adding insulation behind a dense refractory can reduce shell heat loss while raising the operating temperature of the refractory itself. That may affect its strength, wear rate or chemical stability. The best energy result on paper is not useful if it shortens the working lining’s service life.
External conditions matter too. Shell heat loss depends on the shell surface temperature and the surrounding environment, including air movement and heat transfer by radiation. A shell-temperature limit may be driven by equipment integrity, personnel protection or nearby components; those limits should be established before comparing designs. Surface temperature measurements can help identify unusually hot areas, although they do not by themselves establish the condition or remaining thickness of the lining.
Compare expected heat loss on a consistent basis: the same kiln zones, operating temperatures, ambient assumptions and lining condition. Consider both a new lining and a credible worn condition. If the proposed design reduces shell losses, estimate the effect over the expected operating schedule and compare it with material, installation and downtime costs. Do not assume that every unit of reduced shell loss translates directly into the same reduction in fuel use; process controls and other heat flows affect the outcome.
Allow for details that bypass the insulation
Average wall properties do not describe every heat path. Anchors, supports, joints, penetrations and transitions can conduct or leak heat differently from the main lining. Gaps caused by installation, shrinkage or movement may also change local temperatures. Include these details in the evaluation when they occupy a meaningful area, create local hot spots or place temperature-sensitive components at risk.
More insulation also takes space. In an existing kiln, the allowable lining thickness may be constrained by shell diameter, required internal clearance, burner geometry or material flow. A thicker wall that impairs the process or requires major equipment changes may be less attractive than a modest insulation improvement that fits the existing design.
Match the material to the zone, not just the kiln
Different parts of a kiln can require different combinations of insulation, strength and chemical resistance. The following comparison is a starting point for screening material families; individual products vary substantially in composition and performance.
A dense hot face backed by insulation can be appropriate where the process demands a resistant working surface and heat loss remains important. It is not automatically the best arrangement. For example, a fiber-based lining may suit a clean chamber with frequent cycling and limited abrasion, while a zone exposed to moving solids, corrosive deposits or direct impact may require a more robust working surface. In a rotary kiln, the lining must also tolerate shell movement and the mechanical effects of rotation.
Chemical compatibility deserves a separate assessment from temperature capability. Fuel ash, process dust, vapors, slags and deposits can react with or penetrate a lining. The resulting damage depends on composition, temperature and contact conditions. A material suitable for a clean hot-gas atmosphere should not be assumed suitable for the same temperature in a chemically aggressive zone. Adjacent layers should also be checked for compatibility, especially if process constituents can pass through the hot face.
Operating cycles can change the preferred design
For a kiln held near a stable temperature for long periods, steady-state heat loss may dominate the thermal comparison. For a kiln that heats up and cools down frequently, the energy stored in the lining and the time needed to heat it can also matter. A lower-mass lining may reduce stored heat and respond faster, provided it can withstand the process environment and required mechanical duty.
Repeated temperature changes can produce thermal stresses, cracking, spalling or dimensional change. The severity depends on heating and cooling rates, temperature gradients, geometry and how the lining is restrained. Ask suppliers for properties and installation guidance relevant to the actual cycle, rather than treating a maximum service temperature as evidence of thermal-shock resistance.
Cycle-related movement also affects joints, anchors and transitions between materials. A lining that performs well as an isolated product can still fail as an assembly if expansion is restrained or if supporting hardware operates outside its temperature capability. Maintenance planning should account for areas that are difficult to inspect or repair without removing sound material around them.
What to request before making the comparison
A useful technical review puts competing designs on the same operating basis. Provide the kiln geometry, zone temperatures, operating schedule, atmosphere, known chemical exposures, expected abrasion and impact, shell constraints and acceptable downtime. Identify whether each temperature represents a measured condition, a design assumption or an expected excursion.
For each proposed lining, request:
- The layer sequence, installed thickness and expected temperature at each interface, including a worn-lining condition where relevant.
- Thermal conductivity over the applicable temperature range, with the density and test basis associated with the data.
- Temperature limits and information on dimensional stability, strength and resistance to the specified process exposures.
- Installation requirements covering joints, anchors, curing or dry-out where applicable, and allowances for expansion and movement.
- An estimated heat-loss calculation using stated operating and external boundary conditions, together with the assumptions needed to compare alternatives.
Keep uncertain inputs visible in the calculation. If hot-face temperature, remaining lining thickness or deposit formation varies substantially, compare a range of plausible conditions instead of relying on one ideal operating point. A design that performs well only when the working layer remains unworn or the process stays at its lowest expected temperature carries a different risk from one that remains within its limits across the expected campaign.
The final choice is therefore a balance between heat loss and the duty placed on each layer. Select the arrangement that meets the process and shell constraints through the expected operating cycle, then judge the energy benefit against installation, maintenance and campaign-life implications. Where the inputs are uncertain, inspection and temperature measurements during operation can help refine the next lining decision.
Related News
 Ms. Elena RodriguezProcess Equipment Pricing: How to Compare Quotes and Total CostsMaster process equipment comparison pricing: compare supplier quotes, uncover hidden costs, and evaluate lifetime expenses to make a confident buying decision.Nov 17, 2026
 Prof. Marcus ChenGlobal Cement Industry Decarbonization: Key Technologies and Cost BarriersExplore global cement industry decarbonization technologies, cost barriers, and practical investment strategies to cut emissions while protecting competitiveness.Nov 16, 2026
 Structural Material AnalystChoosing Specification Preparation Support for North American ProjectsChoose specification preparation support North America projects can rely on. Compare technical expertise, compliance, interfaces, and supplier acceptance criteria.Nov 14, 2026
 Structural Material AnalystSpecialty Ceramic Extrusion: How Material Properties Affect FormingExplore how ceramic specialized material extrusion is shaped by particle size, binders, and solids loading—and learn to improve forming and reduce defects.Nov 13, 2026
 Ms. Elena RodriguezHigh-Pressure Molding Equipment Prices in Europe: What Affects the Total Cost?Explore high pressure molding equipment price Europe buyers can expect to assess, from tooling and installation to running costs. Compare quotes with confidence.Nov 12, 2026
 Structural Material AnalystChoosing a Vacuum Extrusion System: Capacity, Materials and Vacuum LevelsChoosing a vacuum extrusion system? Compare capacity, material behavior and vacuum levels to improve product quality and select the right equipment.Nov 11, 2026
 Optical Glass Tech FellowGlass Melting Innovations: Comparing Electric and Hybrid Furnace TechnologiesExplore glass melting innovations and compare electric and hybrid furnaces by energy use, emissions, glass quality and operating costs to find the right fit.Nov 10, 2026
 Thermal Energy ArchitectHow Thermal Barrier Technology for Kilns Reduces Heat LossDiscover how thermal barrier technology for kilns reduces heat loss, and learn how to select insulation and assess savings without compromising lining durability.Nov 09, 2026
 Prof. Marcus ChenGlobal Materials Trends: What North American Manufacturers Need to KnowExplore global material trends North America manufacturers need to know, from energy costs and supply chains to lower-carbon materials and smarter investment decisions.Nov 08, 2026
 Thermal Energy ArchitectSelecting Abrasion-Resistant Refractories for High-Wear Kiln LiningsExplore advanced refractory materials abrasion resistant enough for high-wear kiln linings. Compare wear mechanisms, thermal stability, installation and lifecycle costs.Nov 06, 2026
 Dr. Alistair VaughnIndustrial Energy Efficiency Certification: ISO 50001 Requirements for PlantsExplore industrial energy efficiency certification with ISO 50001. Learn how plants define scope, measure performance and prepare credible evidence for audits.Nov 05, 2026
 Ms. Elena RodriguezWhat Is an Industrial Intelligence Database and How Is It Used?Discover how an industrial intelligence database helps researchers map markets, track projects, compare technologies, and assess evidence with confidence.Nov 04, 2026
 Ms. Elena RodriguezIndustrial Material Pricing: How Freight and Order Volume Affect QuotesExplore industrial material pricing and learn how freight, order volume, and inventory costs affect quotes. Compare suppliers and make smarter purchasing decisions.Nov 03, 2026
 Structural Material AnalystSingle- vs. Twin-Screw Extrusion Systems: Which Suits Your Material?Choose the right specialized extrusion systems screw type for your material. Compare single- and twin-screw options to improve quality and control costs.Nov 02, 2026
 Thermal Energy ArchitectChoosing Thermal Barrier Materials for Kilns: Temperature and Heat LossExplore thermal barrier materials for kilns and learn how to balance temperature resistance, heat loss, durability and operating costs when selecting a lining.Nov 01, 2026
 Ms. Elena RodriguezSupplier Reference Platform Pricing: Fees and Contract Terms to CompareCompare supplier reference platform pricing, hidden fees, verification costs and contract terms to choose the right solution for your sourcing team.Oct 31, 2026
 Ms. Elena RodriguezSupplier Comparison Metrics: How to Score Cost, Quality, and DeliveryUse supplier comparison metrics to score cost, quality, and delivery with a practical weighted scorecard. Make more confident equipment sourcing decisions.Oct 30, 2026
 Ms. Elena RodriguezWhat Does Industrial Waste Heat Recovery Cost, and When Does It Pay Back?Understand industrial waste heat recovery cost, from equipment and installation to net savings. Learn how to compare quotes, assess risks, and calculate realistic payback before investing.Oct 29, 2026
 Thermal Energy ArchitectChoosing Industrial Waste-to-Energy Equipment by Waste Moisture and Heating ValueChoose industrial waste to energy equipment by moisture and heating value. Compare technologies, fuel needs, and supplier guarantees to make a confident investment.Oct 28, 2026
 Thermal Energy ArchitectChoosing Industrial Kiln Insulation for High Heat and Repeated Thermal CyclingExplore high temperature industry solutions for kiln insulation under repeated thermal cycling. Compare materials, reduce heat loss, and select the right lining for your operating conditions.Oct 27, 2026




















Related News
- 00
0000-00
How Thermal Barrier Technology for Kilns Reduces Heat Loss - 00
0000-00
Selecting Abrasion-Resistant Refractories for High-Wear Kiln Linings - 00
0000-00
Choosing Thermal Barrier Materials for Kilns: Temperature and Heat Loss - 00
0000-00
Choosing Industrial Waste-to-Energy Equipment by Waste Moisture and Heating Value - 00
0000-00
Choosing Industrial Kiln Insulation for High Heat and Repeated Thermal Cycling
0000-00
Weekly Insights
Stay ahead with our curated technology reports delivered every Monday.